30+ Years of Experience in PCB Design and Manufacturing

Choosing a PCB layout partner is not simply a sourcing decision. It affects signal integrity, thermal behavior, manufacturability, and the number of costly board revisions. The market is growing, but growth alone does not prove a design service is reliable. Grand View Research estimated the global printed circuit board market at USD 76.12 billion in 2023, with projected growth through 2030. That scale raises the stakes for buyers comparing providers across regions.
Small details matter. A poorly placed connector can complicate assembly. An uninterrupted return path can help control electromagnetic interference. IPC-2221 provides a widely used framework for generic printed board design, but a standard cannot replace engineering judgment. PCB design educator Rick Hartley is often associated with the principle, “Current takes the path of least impedance.” It is a compact reminder that layout choices shape real electrical behavior. Buyers should ask how a provider handles stack-up planning, design-rule checks, controlled impedance, and manufacturing feedback—not just whether it delivers files on time.
Evidence counts. Request anonymized project examples, review procedures, and clear revision records. Check whether the team understands your fabricator’s capabilities and can explain trade-offs in plain language. A polished portfolio helps, but it is not proof of consistent results. Even experienced teams miss things; the useful question is how they find and correct them. This guide compares PCB layout design services for global buyers, focusing on technical depth, communication, and practical support from concept through production.
Top PCB Layout Design Services for Global Buyers
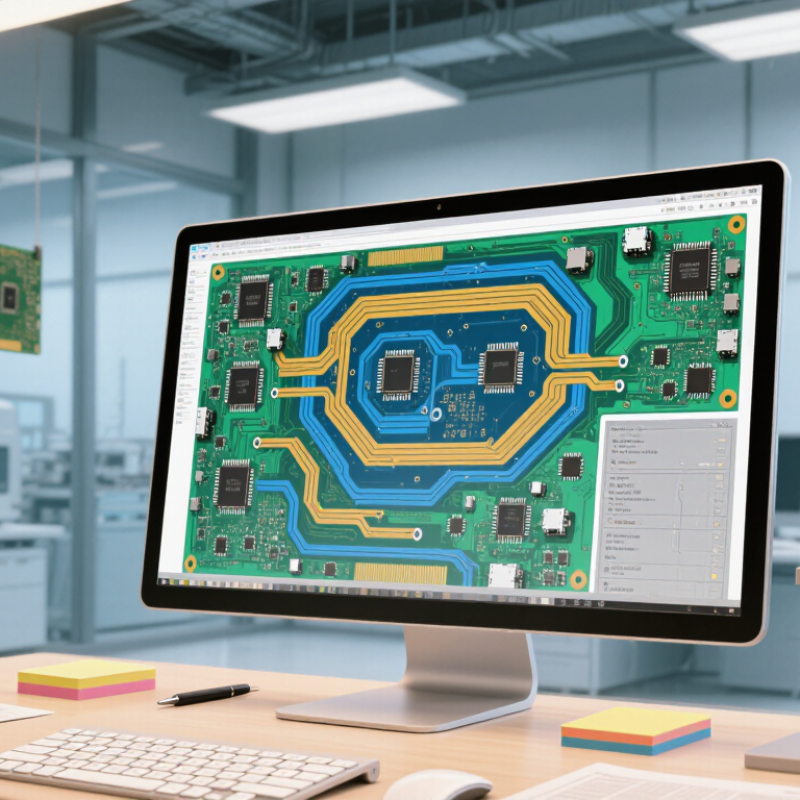
PCB layout services turn circuit requirements into a documented, manufacturable board. Typical work includes component placement, routing, stack-up planning, design-rule checks, and design-for-manufacturing reviews. The service scope should state board layers, controlled-impedance needs, connector locations, and who approves design changes. Grand View Research estimated the global PCB market at about US$76.2 billion in 2024. That scale makes clear why a small layout error can create costly delays across production runs.
A fabrication-ready handoff should include native CAD files, Gerber or ODB++ data, NC drill files, a board outline, and fabrication notes. Add the layer stack-up, copper weights, impedance targets, and a netlist for independent verification. Assembly outputs may include pick-and-place data and a bill of materials, when assembly is in scope. IPC-2221 provides generic design guidance, but the fabricator’s capabilities still matter. A trace width that passes a rule check may not meet the required impedance after stack-up changes. A tidy render is not proof of manufacturability.
Tips: Ask for a DFM report and a final file-readiness review. Confirm units, revision numbers, drill plating, and file naming before release. Keep one detail in mind: approvals can still miss a practical constraint, so review the package with the fabricator before ordering.
| Service Area | Typical Scope | Common Deliverables | Fabrication-Ready Check |
|---|---|---|---|
| Requirements and design review | Review schematics, board dimensions, layer count, component constraints, operating conditions, and manufacturing requirements. | Requirements summary, open-issues list, preliminary stack-up proposal, and design assumptions. | Confirm board outline, units, layer count, copper weights, material requirements, and controlled-impedance needs before routing. |
| Component placement | Arrange components according to functional relationships, mechanical limits, thermal needs, signal flow, and assembly access. | Placement database and review plots, including component locations and reference designators. | Check connector positions, mounting-hole clearances, component orientation, courtyard spacing, and keep-out areas against the mechanical design. |
| Signal and power routing | Route traces and planes while considering connectivity, current capacity, return paths, noise, and routing constraints. | Completed PCB layout database, routed design, and routing or constraint reports where requested. | Run electrical-rule and design-rule checks; review trace widths, clearances, via sizes, plane connections, and unresolved connections. |
| High-speed and controlled-impedance design | Apply constraints for differential pairs, length matching, reference planes, and transmission-line geometry when required by the design. | Constraint summary, impedance-controlled routing details, and stack-up information for the fabricator. | Confirm target impedance and tolerances with the fabricator; final geometry depends on the selected materials, stack-up, and process capability. |
| Design-for-manufacturing review | Check layout features against the selected fabrication process, including spacing, annular rings, solder mask, drill patterns, and board edge features. | DFM findings, revised design files, and a list of agreed process assumptions. | Use the fabricator’s current design rules and resolve flagged issues before releasing production files. |
| Design-for-assembly review | Review component spacing, polarity markings, soldering access, panelization considerations, and assembly documentation needs. | Assembly review notes and, if included in scope, assembly drawings or placement data. | Verify that assembly outputs match the released PCB revision; assembly services and PCB fabrication are separate deliverables unless specifically included. |
| Fabrication data package | Prepare the board-layer and drill data needed for a PCB manufacturer to interpret the finished design. | Gerber files (commonly Gerber X2) or IPC-2581 data, NC drill files, board outline, and fabrication notes. | Include all required copper, solder-mask, legend, and outline layers; identify drill units, plating requirements, and finished board thickness. |
| Stack-up and material information | Document layer order, dielectric construction, copper thickness, board thickness, and any impedance requirements. | Stack-up drawing or table, material notes, and impedance targets where applicable. | Have the fabricator review the stack-up before production, especially for controlled impedance, special materials, or nonstandard thicknesses. |
| Assembly and procurement data | Provide component and placement information when assembly support is part of the project scope. | BOM, pick-and-place or centroid file, assembly drawing, and component polarity or orientation notes. | Check reference designators, units, coordinate origin, rotation conventions, and revision consistency with the assembly provider. |
| Release and revision control | Organize final files so the buyer and manufacturing partners can identify the approved design revision. | Release manifest, revision identifier, source design files if agreed, and a compressed fabrication package. | Open and inspect the exported files, confirm they match the approved layout, and remove obsolete or ambiguous revisions from the release package. |
Buyer tip: Agree on the PCB design tool, file formats, stack-up ownership, fabrication rules, and included review rounds before work begins. Final manufacturing acceptance should be confirmed with the chosen fabricator.