Choosing a custom plastic housing manufacturer can shape a product’s cost, reliability, and launch schedule. A smooth sample is encouraging, but it does not prove that every production part will fit. Ask how the supplier controls dimensions, resin selection, tooling, and inspection. Small details matter: a screw boss that cracks, a thin wall that warps, or a connector opening shifted by one millimeter can delay assembly. These are practical questions, not paperwork.
Look beyond the quoted unit price. Review the manufacturer’s relevant project experience, equipment, quality checks, and ability to explain design trade-offs in plain language. Request material data and sample parts, then compare them with your drawings and operating conditions. A capable partner should discuss mold maintenance, expected production volumes, and what happens when a defect appears. Clear answers build confidence. Vague promises do not.
There is no perfect checklist. A supplier that suits a high-volume enclosure may not fit a short-run product with frequent design changes. That distinction is easy to miss. Share realistic requirements, including target quantities, finish, tolerances, and delivery expectations, before comparing proposals. This guide outlines how to assess a custom plastic housing manufacturer with evidence rather than sales claims. It also considers where buyers can make stronger decisions—and where a second review may still be worthwhile.
Start with the housing’s job, not its appearance. Describe what it encloses, how users handle it, and where it will operate. An outdoor sensor may need sealed seams and UV-resistant material, while a desk enclosure may prioritize finish and access. Record heat, moisture, impact, cleaning agents, and expected service life. Be specific. Photos, sketches, and a rough, hand-sized mock-up can expose unclear assumptions early.
Translate those conditions into measurable requirements: overall dimensions, wall thickness, mounting points, openings, color, texture, and acceptable gaps. Identify critical tolerances around connectors, buttons, and mating halves; a small mismatch can complicate assembly. State whether the part needs snap fits, inserts, or post-mold machining. Not every detail is settled. Mark open questions rather than presenting guesses as fixed specifications.
Set production goals too. Share expected annual demand, launch timing, prototype quantity, and likely growth. Ask for pricing at realistic volume steps, along with tooling ownership, lead times, inspection methods, and acceptable defect criteria. These inputs help a manufacturer assess whether the design suits the intended process and budget. Material choice or late changes can alter cycle time and cost; revisit targets after reviewing samples.
Define your housing requirements and production goals: material choice affects tooling shrinkage and therefore dimensional planning.
Typical molding shrinkage ranges for selected plastics are shown as percentages. Actual shrinkage depends on the resin grade, part geometry, mold design, and processing conditions. Confirm the exact grade’s data sheet with your manufacturer when setting tolerances and production targets.
How to Choose a Custom Plastic Housing Manufacturer
Compare Materials, Processes, and Manufacturing Capabilities
Start with the housing’s working conditions: heat, impact, sunlight, cleaning fluids, and expected service life. ABS can suit rigid indoor enclosures; polycarbonate may be preferable where impact resistance matters. Compare technical data sheets, not just resin names. Check operating temperature, shrinkage, UV performance, and any required flame-retardant rating. A sample part can reveal problems that a spreadsheet misses.
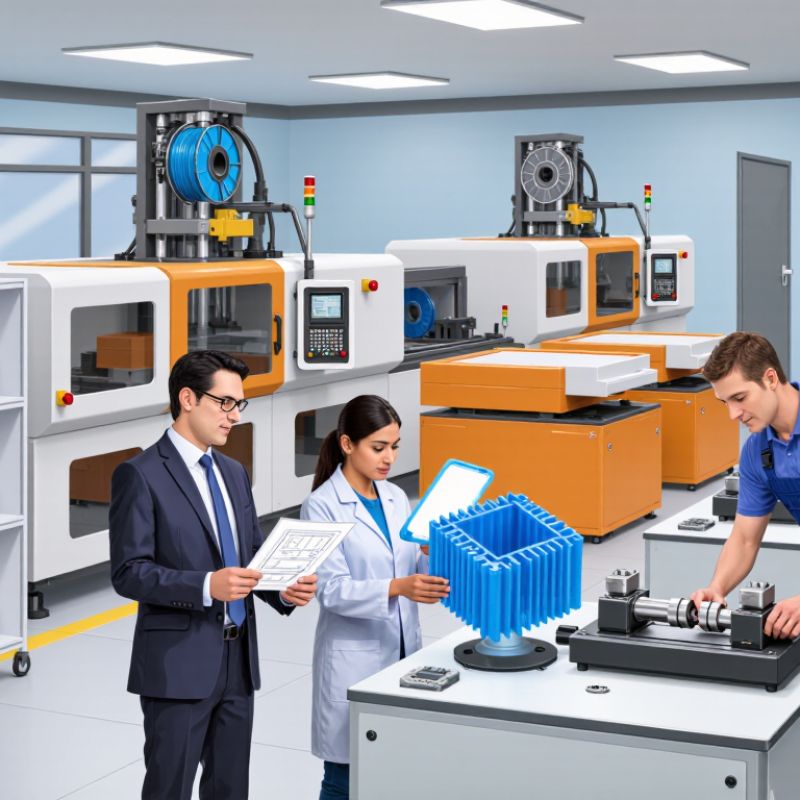
Then match the design to the process. Injection molding suits repeat production, but tooling costs and lead times need careful review. Thermoforming or CNC machining may fit lower volumes or early prototypes. Ask how the manufacturer controls wall thickness, draft angles, dimensional tolerances, and cosmetic defects. PlasticsEurope’s Plastics—The Fast Facts 2024 reports global plastics production of 413.8 million tonnes in 2023. Scale is substantial, but it does not guarantee consistent parts. Request examples of comparable housings and inspection records.
Manufacturing capability matters beyond the molding machine. Check whether the supplier can support mold-flow analysis, tooling changes, assembly, and measured first-article samples. The OECD’s Global Plastics Outlook (2022) reports that only 9% of plastic waste was recycled in 2019. If recycled resin is part of the specification, request material traceability and test molded samples for fit and impact performance. I still find resin substitutions easy to overlook. A small change can affect snap fits.
| Option | Key characteristics | Common housing applications | Process fit | Capabilities to verify with the manufacturer | Important trade-offs and questions |
|---|---|---|---|---|---|
| ABS (Acrylonitrile Butadiene Styrene) | Good impact resistance and toughness; readily colored and commonly used for molded parts. Heat and UV performance depend on the specific grade. | Indoor equipment enclosures, appliance housings, control panels, and consumer-product shells. | Injection molding is widely used. Sheet-grade ABS can also be thermoformed for suitable part designs. | Ask about experience with the intended ABS grade, mold design, draft and wall-thickness review, color matching, and cosmetic-surface inspection. | Confirm operating-temperature and outdoor-exposure requirements. Specify whether flame-retardant or other regulated grades are needed. |
| Polycarbonate (PC) | High impact strength and good transparency in suitable grades; heat resistance is generally higher than that of general-purpose ABS. Chemical compatibility varies. | Clear covers, protective guards, instrument housings, and impact-resistant enclosures. | Injection molding is common; thermoforming is possible with appropriate sheet stock and part geometry. | Check capability for drying moisture-sensitive resin, controlling optical quality where needed, and managing molded-part stress and appearance. | Review resistance to the actual cleaners, oils, or chemicals used. Ask whether UV-stabilized or flame-retardant grades are required. |
| PC/ABS blend | Combines properties of polycarbonate and ABS; often selected for a balance of impact performance, processability, and heat resistance. Exact properties vary by grade. | Electronic equipment cases, automotive interior components, and general-purpose durable enclosures. | Primarily injection molded for production housings. | Confirm the supplier can process the specified blend consistently and control shrinkage, weld lines, surface finish, and dimensional tolerances. | Request grade-specific data rather than assuming all blends perform alike. Validate compatibility with coatings, fasteners, and the service environment. |
| Polypropylene (PP) | Low density, good chemical resistance to many substances, and fatigue resistance useful for living hinges. Stiffness and impact behavior depend on grade and temperature. | Fluid-handling covers, lightweight housings, hinged enclosures, and parts exposed to many common chemicals. | Injection molding is common; the design should account for material shrinkage and warpage. | Ask about experience with PP grade selection, gate and cooling design, warpage control, and dimensional inspection. | Check low-temperature impact needs, rigidity, and dimensional stability. Confirm chemical resistance against the exact substances and exposure conditions. |
| Nylon (PA) | Good strength and wear resistance in many grades; absorbs moisture, which can affect dimensions and mechanical behavior. Glass-fiber reinforcement changes stiffness and shrinkage. | Structural brackets, rugged equipment housings, and enclosures with integrated clips or load-bearing features. | Injection molding is common. Resin drying and grade-specific processing control are important. | Verify resin-drying procedures, experience with reinforced grades if applicable, and inspection methods that account for moisture-related dimensional changes. | Define humidity and temperature conditions, dimensional tolerances, and load requirements. Check whether exposed glass fibers or surface finish are concerns. |
| Injection molding | Suitable for repeatable production of complex parts after tooling is made; tooling cost and lead time can be significant. | Medium- to high-volume housings, snap-fit parts, and designs with ribs, bosses, or integrated features. | Thermoplastic pellets are melted and injected into a mold, then cooled and ejected. | Review mold-design support, tool ownership terms, mold maintenance, process validation, dimensional measurement, and production-capacity planning. | Ask for a design-for-manufacturing review and a clear plan for prototypes, tooling approval, first-article inspection, and production changes. |
| Thermoforming | Forms heated plastic sheet over or into a mold; tooling can be simpler than injection tooling for some parts, but detail and feature geometry are more limited. | Large, relatively shallow covers, panels, trays, and low- to medium-volume enclosures. | Plastic sheet is heated and formed using vacuum, pressure, or a combination of methods; excess material may require trimming. | Check sheet-material options, forming-area limits, trim-fixture capability, repeatability, and finishing or assembly services. | Confirm acceptable wall-thickness variation, edge quality, and achievable detail. Review how openings and mounting features will be made. |
| CNC machining | Produces parts from plastic stock with no dedicated production mold; useful for prototypes and low quantities, but material waste and cycle time can be higher. | Functional prototypes, small batches, precision parts, and designs needing late-stage adjustments. | Computer-controlled cutting removes material from sheet, plate, or block stock. | Ask about available stock materials, achievable tolerances for the specific geometry, surface-finish options, and inspection equipment. | Check for tool-access limits, corner radii, and part cost at the expected quantity. Machined properties can differ from molded-part behavior. |
| Manufacturer selection checklist | A capable supplier should be able to discuss the intended environment, resin grade, part geometry, annual volume, appearance, tolerances, and compliance needs before quoting. | Request evidence of relevant process experience, design-for-manufacturing feedback, quality-control procedures, material traceability where required, and a defined sampling or first-article approval process. | Compare total project cost, including tooling, validation, finishing, assembly, packaging, lead time, and change management—not unit price alone. | ||
How to Choose a Custom Plastic Housing Manufacturer
A capable manufacturer should help refine the design, not just quote the drawing. Ask for feedback on wall thickness, draft angles, snap fits, and mounting bosses. These details affect tooling, strength, and assembly. A useful review considers the complete product: cable routes, nearby heat sources, and how a technician will open the housing. Details matter. Request marked-up drawings or specific recommendations, rather than general assurances.
Prototyping should answer clear questions. A 3D-printed sample can reveal awkward hand clearance or a connector that sits too close to a wall. It may not predict the flexibility or finish of a molded part, though. Discuss which prototype method suits each test, such as checking fit, screw torque, or access to controls. Small trials help. A polished CAD file can still hide a practical flaw; it is easy to overlook one until parts are handled.
Quality controls need to be visible and relevant to the housing. Ask how incoming resin is identified, which dimensions are measured, and how inspection results are recorded. Critical features might include latch height, hole spacing, and mating-surface flatness. Request a sample inspection report and learn what happens when a measurement falls outside tolerance. A checklist alone is not proof of consistency. I would also clarify how design changes are approved, since even a small revision can affect fit, tooling, or inspection criteria.
When choosing a custom plastic housing manufacturer, compare more than the unit price. Ask for a breakdown covering material, tooling, setup, packaging, and inspection. A low part cost can hide a large mold charge or a minimum order that exceeds your needs. Check which resin grade and color assumptions the quote uses. Small details matter.
Lead times need the same scrutiny. Ask when the schedule begins: after deposit, drawing approval, or final sample sign-off? Request separate estimates for tooling, first articles, and production. A date without these milestones is hard to evaluate. Confirm how design changes affect the schedule. Even a well-planned project can slip when a fitting or wall thickness changes late.
Communication practices often reveal how manageable that risk will be. Ask who owns your project and how often you will receive updates. A useful update names the completed step, the next action, and any open decision. Keep drawings and approvals in writing. That helps. If replies are vague before an order, they may stay vague later; still, response speed alone does not prove manufacturing skill. Agree on a realistic update rhythm, and leave a buffer for sample revisions. The buffer may feel excessive until it is not.
Verify Compliance, Reliability, and Ongoing Support
Ask for current quality certificates, then check that their scope covers the actual molding site and processes. ISO’s 2022 Survey recorded 1,265,216 valid ISO 9001 certificates worldwide. That number signals broad adoption, not guaranteed performance. Request recent audit findings, inspection records, and sample dimensional reports. For a housing, compare measurements around screw bosses, snap fits, and connector openings against the approved drawing. Small deviations can create assembly problems. Ask how the supplier documents resin grades, colorants, and process changes. A certificate alone is not enough.
Material accountability matters, too. The OECD’s Global Plastics Outlook reports that global plastics production reached 460 million tonnes in 2019, nearly double its 2000 level. Ask manufacturers to identify resin sources and provide traceable material records for each production lot. For housings with specific environmental or performance requirements, verify that the chosen material and test evidence match the intended use. Then test the support system: who responds when a tool needs adjustment, a shipment slips, or a design changes? Get response times, escalation contacts, spare-tool plans, and change-approval steps in writing. Try a real scenario. A polished promise is easy; a documented response is more useful. I would still inspect early production parts myself. Paperwork can miss the detail.